-
 +86 13683394660
-
 bjjyInternational@yeah.net
Welcome to the official website of Beijing Jiyuan Zineng (International) Environmental Technology Co., Ltd.
 +86 13683394660 bjjyInternational@yeah.net
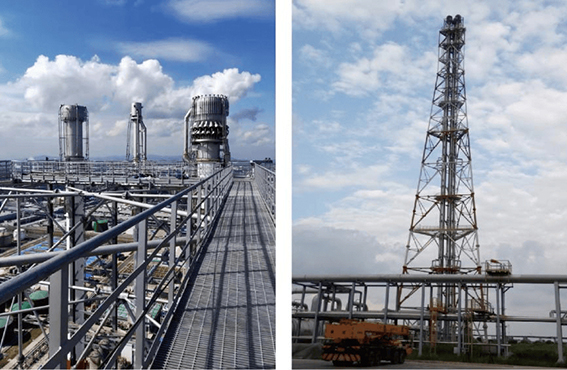
Core Flare Equipment-Elevated Flare System
Application:
Large refineries — suitable for both steady-state normal operation and large-volume waste gas discharge under accidental / emergency conditions.
Core configuration:
Features an efficient combined flare head and premixed acid-gas flare burner, specially designed for refinery sour gas and complex hydrocarbon-containing waste gases.
Core Advantages
Burning efficiency of ≥ 99.9% and pollutant removal rate of ≥ 99.99%, suitable for treating the high-sulfur off-gas typical of Middle East refineries.
Features energy-efficient pilot lights/burners consuming just 1.5–3.0 Nm³/h of gas per unit — more than 60% energy savings versus traditional units, greatly lowering fuel operating expenses.
Wind load resistance of 36 m/s, able to withstand gales and blowing sand/dust, ensuring stable performance in extreme weather conditions.
Robust handling capability — maximum accident-flare gas flow of 112,477 Nm³/h and a flare stack/derrick reaching up to 150 m, fully satisfying the emergency depressurization and relief requirements of major refineries.
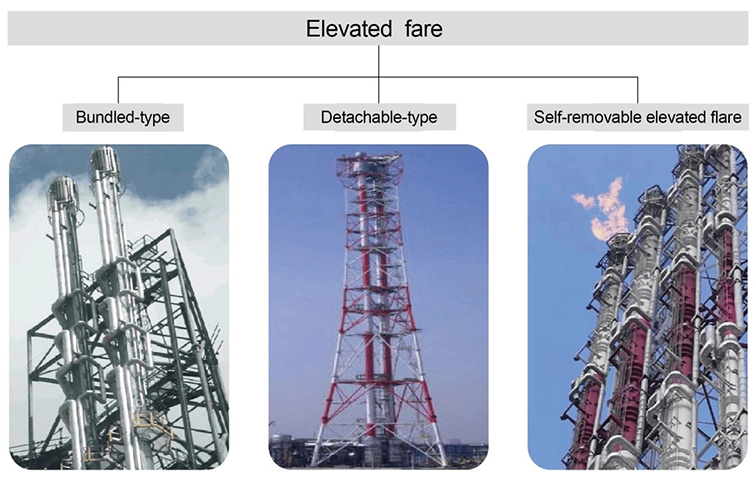
Product categories: Bundled-type, detachable-type, and self-removable elevated flare systems.
Core Flare Equipment-Ground Flare System
Application scope:
Refinery projects where stringent controls on visual landscape and light pollution are required.
Core characteristics:
Flames are completely confined inside the combustion tower — no light pollution, no black smoke. The matrix-style burner layout delivers 100% smokeless combustion, keeping nitrogen oxide (NOₓ) emissions well under the regulatory limit.
Application versatility:
It handles complex, hydrogen-rich, and sulfur-rich exhaust and is constructed with specialized anti-corrosion materials for high-temp, high-salinity environments, offering a 15+ year lifespan and reduced upkeep.
Safety Assurance:
MSI™ Indirect Continuous Ignition System: Boasts a 100% first-time ignition success rate, coupled with a burst disc bypass to handle sudden high-pressure exhaust surges.
Negative Pressure Operation (100 Pa): Prevents high-temp flue gas escape, fully compliant with rigorous Middle East industrial safety standards.
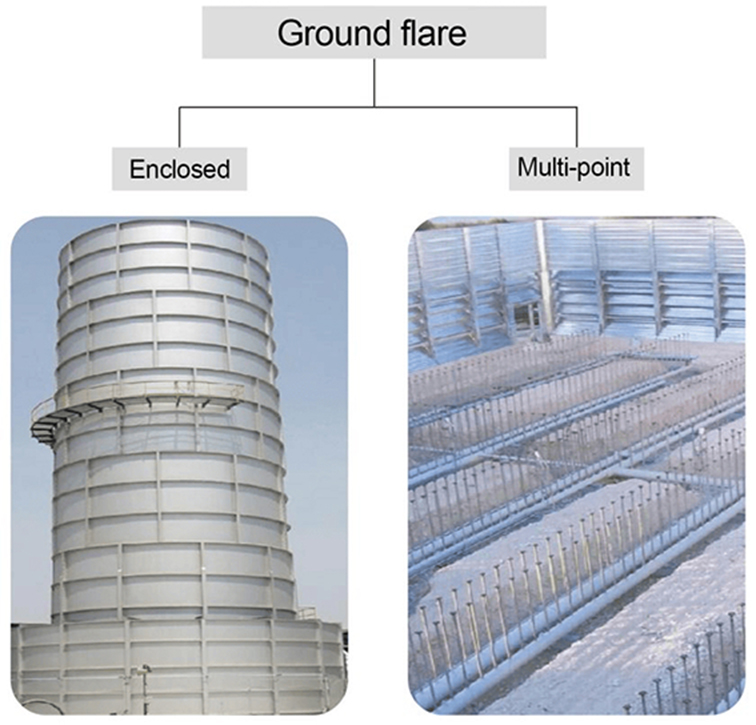
Product Categories: Enclosed ground flares and multi-point ground flares; capable of integration with elevated flares to form a combined high-altitude and ground flare system.
Supporting Energy-Saving and Recovery Technologies
Waste Heat Recovery System (WHRS)
Proprietary L-type cascaded flue gas waste heat recovery technology: Converts flare combustion heat into 1.0–9.8 MPag saturated steam, which is directly supplied to refinery production processes. This reduces steam procurement costs, with annual energy savings for a mid-size refinery exceeding USD 1 million.
Low-NOₓ Combustion Optimization
Low-NOₓ Combustion Optimization: Fuel staging + air staging patents combine with low-NOₓ burners to inhibit NOₓ generation. NOₓ ≤ 50 mg/m³ — fully compliant with rigorous low-NOₓ emission standards.
VOCs Co-treatment / VOCs Co-control
Rotary RTO/RCO system: Handles VOCs from loading operations & tank emissions; purifies exhaust up to 3,603 mg/Nm³ at ≥99% efficiency — fully compliant with Middle East VOCs control standards.
Sulfur Recovery Synergy
Recovers sulfur from H₂S-rich tail gas while simultaneously treating main emissions, converting pollutants into a marketable sulfur byproduct to achieve both emission reduction and revenue generation.
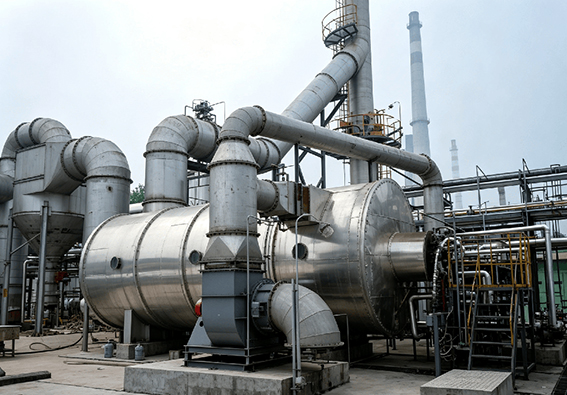
Typical Cases
Case Studies:
This technology has been successfully deployed in over 100 petrochemical projects, covering 25 provinces and municipalities across China, serving globally recognized clients including PetroChina, Sinopec, and BASF-YPC Company Limited. The flare systems operate stably in major projects such as Xinjiang Tianye’s 1 Mt/y ethylene glycol facility and Hami Guanghui’s 400 kt/y ethylene glycol facility, demonstrating extensive experience in treating high-sulfur, high-load exhaust. The technology can be directly transferred to refinery projects in the Middle East.