-
 +86 13683394660
-
 bjjyInternational@yeah.net
Welcome to the official website of Beijing Jiyuan Zineng (International) Environmental Technology Co., Ltd.
 +86 13683394660 bjjyInternational@yeah.net
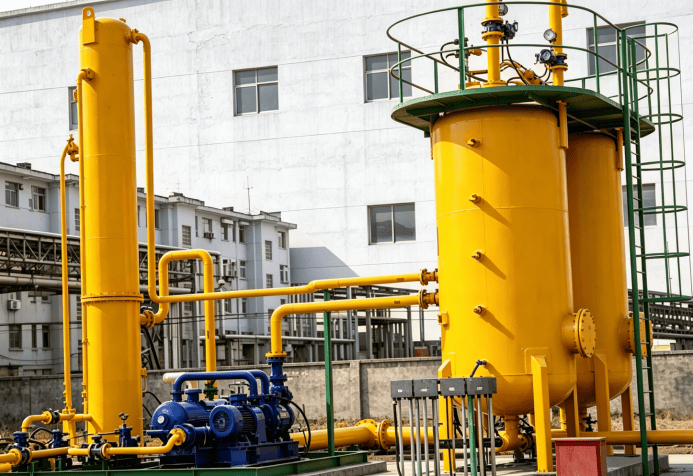
Core Technologies-Pressure Swing Adsorption (PSA+ Absorption Technology
Applications:
High-efficiency recovery of high-concentration oil and gas; oil depot tank farms and high-concentration emission conditions.
Core principle:
Oil & gas flows into a two-tower adsorption system and is purified over dedicated activated carbon, with clean air emitted compliantly. Once saturated, the carbon is desorbed under high vacuum to release concentrated oil & gas, which is fed to a vertical absorber for countercurrent contact with a specialized absorbent. The oil & gas dissolves into rich oil, a product directly marketable as commercial oil.
Core Advantages
Suitable for Middle East crude oil, gasoline, and mixed hydrocarbon fractions — achieves ≥ 98% adsorption efficiency with thorough desorption leaving no residual.
Energy-efficient vacuum desorption: Designed for Middle East power costs — simple O&M and low-frequency consumables replacement.
Modular design: Small footprint that fits into existing site layouts, enabling short renovation/retrofit cycles.
Core Technologies-Condensation Recovery Technology
Applications
Remote oil depots, small loading areas, and projects with no adsorbent loss requirements.
Core principle
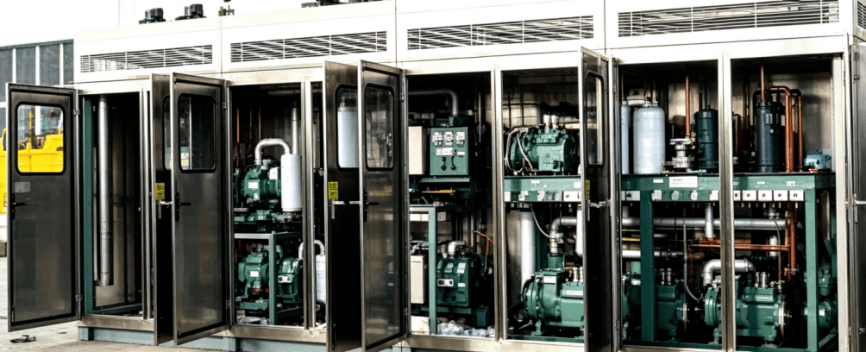
Using a three-stage cascade condensation process, stage 1 at 35℃ removes most heavy hydrocarbons; stage 2 at −25 to −35℃ recovers intermediate hydrocarbons; stage 3 at −65 to −75℃ captures light hydrocarbons. The temperature gradients are tailored to the condensation traits of each component. Condensed liquid oil is directly recycled back to the tank, and tail gas meets emission standards.
Core Advantages
Staged condensation: Recovery efficiency ≥ 95%, with light hydrocarbon recovery superior to conventional single-stage condensation.
Explosion-proof, high-temperature-resistant refrigeration unit: Tolerates extreme heat above 50℃, delivering stable and reliable performance.
No adsorbent consumption: Minimal O&M costs, well suited to remote Middle East locations.
Core Technologies-Condensation-Adsorption Combined Process
Applications
Projects with strict emission requirements — refineries, terminals, and large loading areas (the preferred solution across the Middle East).
Core principle
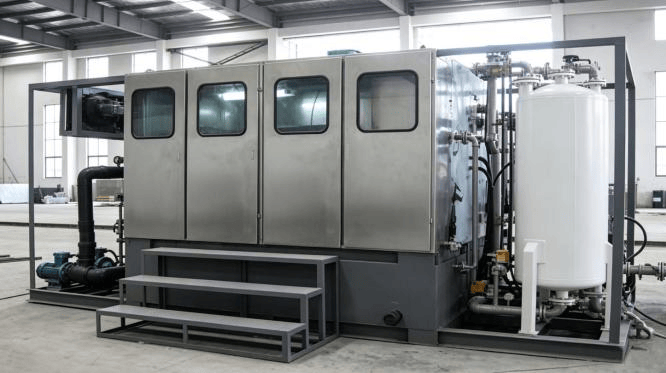
High-concentration oil & gas first passes through a three-stage low-temperature condensation unit, condensing over 90% of organic compounds into recoverable liquid. The remaining low-concentration residual gas then enters a PSA (pressure swing adsorption) unit for deep purification, while the concentrated tail gas from adsorption/desorption is recycled to the front end of the condensation stage for cyclic treatment — delivering both ultra-low emissions and system-wide energy savings.
Core Advantages
High recovery performance:
Achieves ≥ 99% recovery with an emission concentration of ≤ 20 mg/m³, complying with the most stringent VOCs limits across the Middle East.
Energy-saving and integrated:
Energy consumption is reduced by over 30% compared with pure condensation; skid-mounted integrated equipment requires no on-site assembly.
Integrated four-unit system:
Combines low-temperature condensation, adsorption, recovery, and intelligent control — enabling unattended operation and suited to the Middle East’s high manpower-cost conditions.
All-Scenario Solutions
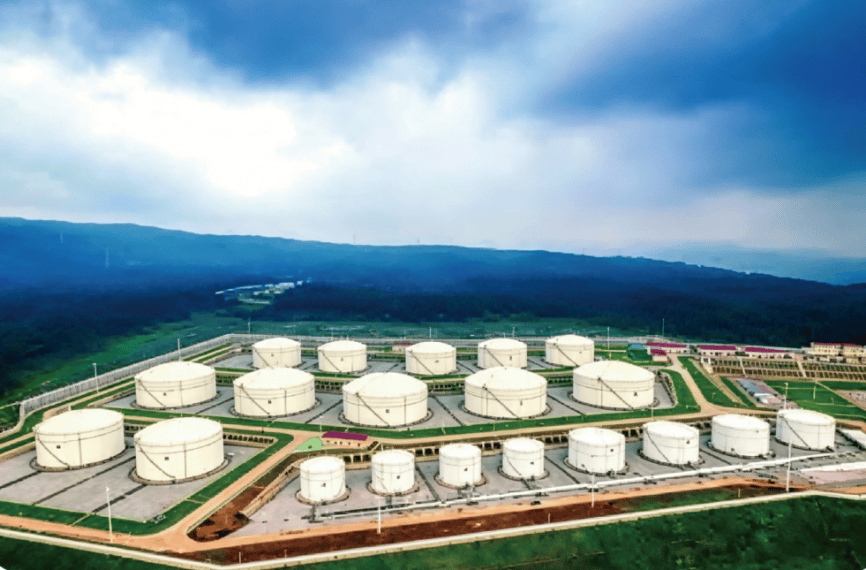
Tank Farm Vapor Recovery
Pain points: Fugitive/unorganized emissions from storage tank breathing — both normal and thermal breathing — result in product loss and VOC contamination.
Solution: Using a combined condensation, adsorption/pressure-swing adsorption, and absorption process to capture and treat tank breathing vapors in real time — a single tank can recover dozens of tons of oil annually.
Compatible media: Gasoline, crude oil, kerosene, diesel, naphtha, mixed hydrocarbons, and more.
Truck Loading Station Vapor Recovery
Pain point: Vapor fugitive emissions and product loss during road and rail loading operations.
Solution: A closed-loop system links the sealed loading arm to the recovery unit, triggering vapor recovery the moment loading starts. The recovered liquid oil is sent back to the tank farm, ensuring sealed, zero-emission recovery throughout the loading operation.
Highlight: 100% system synchronization rate, with no impact on loading efficiency.
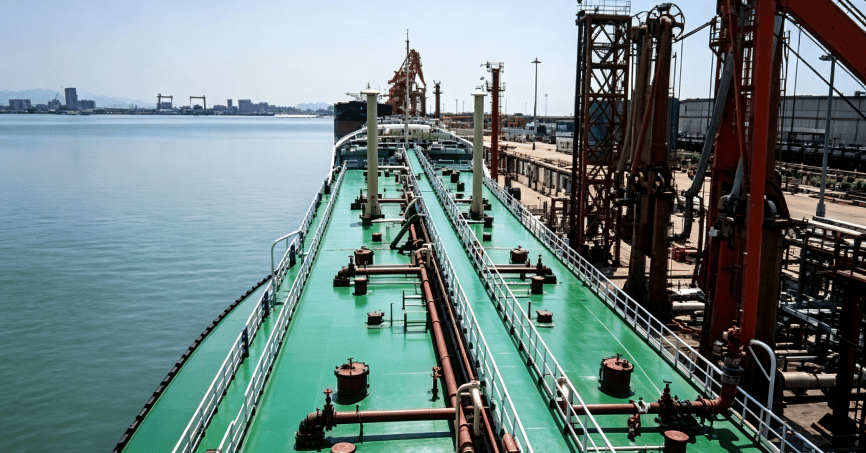
Marine Terminal Vapor Recovery
Pain points: Vapor escape at the ship-shore interface during tanker loading and unloading, plus the high salt-spray, corrosive environment typical of marine terminals.
Solution: A fully integrated ship-shore enclosed recovery system that includes the vapor collection line, ship-shore interface facilities, and onshore processing equipment; it is configured with explosion-proofing, leak detection and monitoring, and anti-corrosion components resistant to sea-wind salt spray.
Advantage: Engineered for the harsh, high salt-spray and strong sea-wind environment of Middle East terminals, delivering safe and dependable operation.
Media Treatment Range
Media treatment range: Capable of treating a full spectrum of hydrocarbon media, including Category C hydrocarbons, aromatics, alcohols, ethers, ketones, and esters, covering refined product and chemical storage tank farms as well as loading/unloading operations.
Typical Cases
The technology has been successfully applied to the oil & gas recovery projects of several large international petroleum enterprises. Partial typical cases are listed below:
Sinopec Maoming Branch — Oil Loading Workshop: 500 Nm³/h oil & gas, condensation + membrane process.
Yanchang Petroleum Group, Yan'an Refinery: 1000 Nm³/h vapor recovery using condensation + adsorption technology.
Shandong Dongming Petrochemical Group, Railway Loading Facility: 500 Nm³/h vapor recovery using condensation + adsorption technology.
CNOOC Shandong Haihua Petrochemical Company: 400 Nm³/h vapor recovery using condensation + adsorption technology.
Fuda Petrochemical Storage Terminal, Nansha, Guangdong: 800 Nm³/h vapor recovery using condensation + adsorption technology.
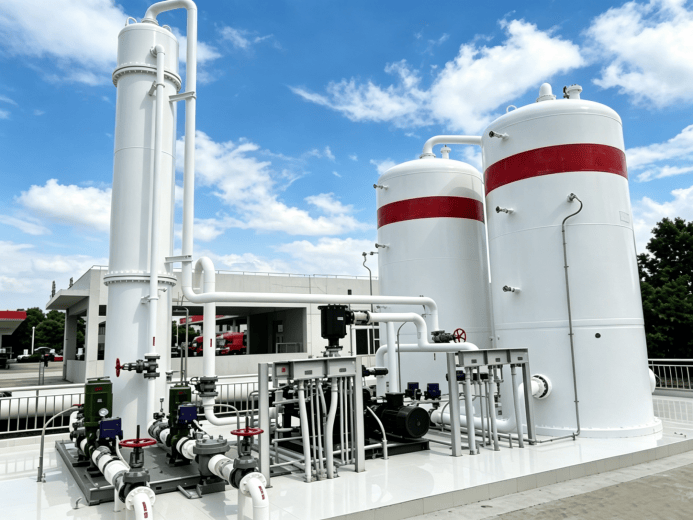
Oil Terminal Vapor Recovery
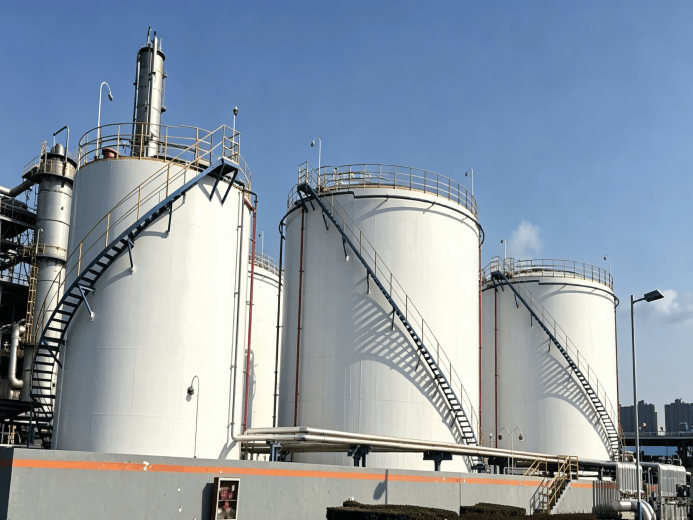
Storage Tank Farm Vapor Recovery
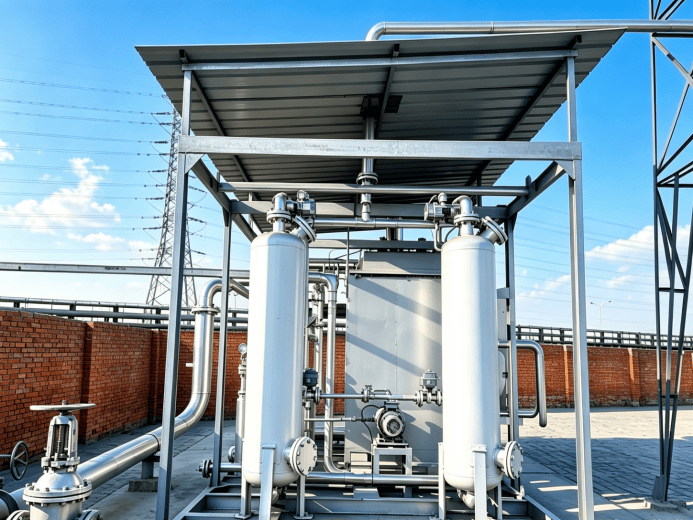
Truck Loading Station Vapor Recovery
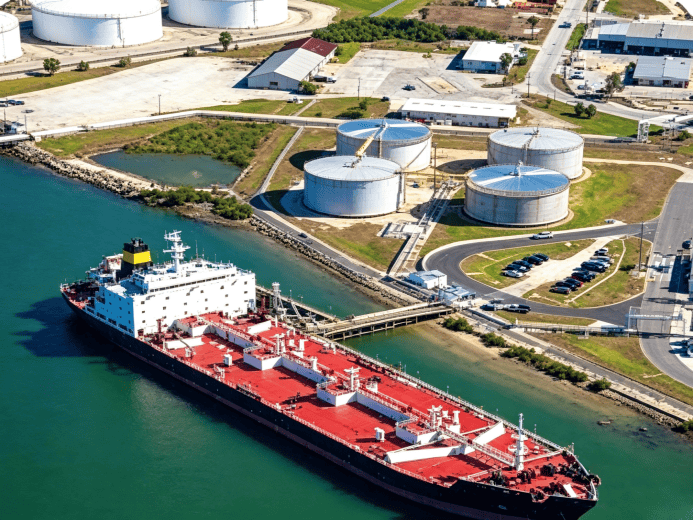
Marine Terminal Vapor Recovery